How fiber dispersion affects wet-laid nonwoven pore uniformity
Fiber dispersion affects wet-laid nonwoven pore uniformity by controlling where fibers accumulate as the sheet forms. When fibers arrive at the forming surface as persistent flocs, they create dense regions alongside relatively open areas. Those open areas can contain larger connected flow paths, allowing a small portion of the sheet to carry disproportionate airflow. A medium can therefore meet its average basis-weight and permeability targets while still showing uneven particle penetration or inconsistent pressure drop across samples.
Better dispersion generally reduces this source of variation, but it does not guarantee a narrow pore-size distribution. Fiber diameter, drainage, orientation, bonding, and consolidation also determine the finished structure. For technical evaluation, the useful question is whether dispersion is limiting pore consistency—and whether a proposed correction improves the finished medium without damaging fibers or disrupting its intended architecture.
How flocs become uneven flow paths
In Wet-Laid Nonwoven Technology, fibers are suspended in water, delivered to a forming zone, and retained while water drains through a supporting surface. A well-distributed suspension gives individual fibers more opportunity to form a spatially consistent network. Flocculated fibers reach the forming zone as groups, leaving local differences in fiber mass and spacing that subsequent processing may preserve.
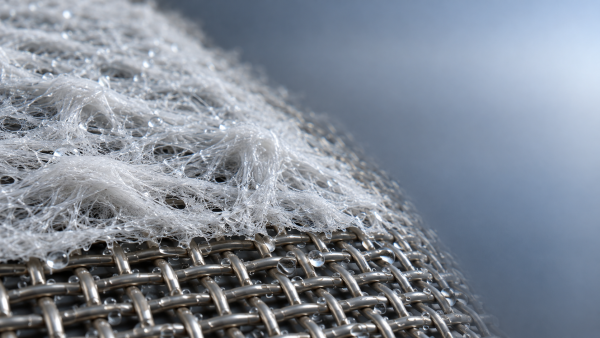
A floc does not simply create one large pore. Its interior may contain tightly packed fibers and small openings, while its edges border areas with less fiber coverage. The resulting sheet can contain both restrictive regions and easier flow paths. Through-thickness connectivity matters: a visible surface opening may lead to a constriction deeper in the web, while several less obvious openings may connect into a preferential passage.
Airflow follows the resistance of these connected paths. Relatively open regions can carry more flow and experience higher local velocity, potentially reducing particle capture under otherwise comparable conditions. Dense regions contribute resistance without necessarily compensating for penetration elsewhere. This explains why an acceptable average air-permeability result cannot establish pore uniformity.
The relationship also depends on the filtration mechanism. Fibrous filters capture particles through interactions with fibers throughout the structure; they do not behave simply as sieves with a single cutoff size. Pore measurements help describe the network, but filtration efficiency must still be measured at relevant operating conditions.
Which dispersion conditions deserve attention?
Fiber geometry and wetting establish the operating window
Long, slender fibers are more prone to mechanical entanglement than shorter fibers under otherwise comparable suspension conditions. Their flexibility, surface condition, and concentration affect whether contacts separate during mixing or persist as bundles. A recipe that disperses a relatively coarse, short fiber successfully may perform differently after the introduction of a finer or longer component.
Synthetic fibers introduce an additional challenge when their surfaces resist wetting. Incomplete wetting can preserve bundles or associate fibers with entrained air. Surface finishes and wetting agents can assist dispersion, but their compatibility with the rest of the formulation matters. Changes in finish chemistry may also influence foam, binder interaction, and drainage.
Mixed-fiber systems need particular care. Coarse support fibers and fine capture fibers may respond differently to the same preparation conditions. A suspension can look reasonably uniform while the fine component remains clustered or becomes unevenly retained during formation. Inspection should therefore consider the distribution of individual fiber populations, especially when a small fine-fiber fraction contributes substantially to filtration performance.
Consistency, chemistry, and mixing act together
Higher suspension consistency increases opportunities for fiber contact and can encourage flocculation. Dilution can help fibers separate, although it changes water handling and drainage demands. Comparisons between trials should record consistency at relevant process locations; a preparation-tank value alone may not describe conditions near the headbox.
Water chemistry changes how fibers and additives interact. Depending on the formulation, pH, dissolved ions, dispersants, and retention aids can affect suspension stability. An additive that improves retention may also promote aggregation. Its addition point and mixing history can determine whether that aggregation supports the process or produces persistent formation defects.
Mixing must provide enough energy to wet and separate fibers, with residence time suited to the material. Increasing agitation indefinitely is a poor control strategy. Excessive mechanical action can shorten susceptible fibers, generate fines, entrain air, or destabilize other formulation components. Improved visual dispersion obtained through fiber damage may produce a different pore structure rather than a better-controlled version of the intended one.
Dispersion can also deteriorate after preparation. Fibers separated in a tank may reaggregate in transfer lines, low-velocity regions, or the approach-flow system. Sampling close to the forming zone is consequently more informative than relying entirely on a well-dispersed laboratory beaker.
Separate dispersion defects from formation and finishing effects
The wet web continues to change after the suspension reaches the forming surface. Drainage moves fibers and fines, the developing fiber mat alters local resistance, and pressure or suction influences deposition. A uniformly dispersed furnish can still form an uneven sheet if flow distribution or drainage is poorly controlled.
Fiber orientation introduces another distinction. Fibers may be well separated but preferentially aligned by flow. The resulting network can have directional properties without showing obvious flocs. Likewise, a gradient medium can intentionally vary fiber size or density through its thickness while maintaining good lateral uniformity. Such designed variation should be distinguished from random open regions across the sheet.
Bonding and consolidation further alter the openings established during formation. Binder can occupy pore space or migrate unevenly during drying. Thermal bonding and mechanical compression change fiber contacts, thickness, and local packing. Lamination can add resistance or create bond patterns that affect the measured composite. A finished-media pore result therefore cannot, by itself, identify dispersion as the cause.
Stage-by-stage comparisons help locate the problem. Where practical, examine formation before major consolidation, then compare the same formulation after bonding or lamination. Record basis weight, thickness, and test conditions alongside pore measurements. If a large change appears only after finishing, adjusting suspension chemistry may leave the dominant cause untouched.
What measurements can establish pore uniformity?
No single measurement covers dispersion, pore geometry, and filtration performance. A useful evaluation links evidence from the suspension, the sheet, and the finished medium. Each measurement should answer a specific question rather than serve as a general quality score.
- Suspension inspection: Microscopy or suitable imaging can reveal persistent bundles and differences between fiber populations. Sample preparation must avoid dispersing flocs that existed in the process or creating new ones during handling.
- Formation assessment: Transmitted-light imaging or local basis-weight mapping can identify spatial variation. Optical contrast also depends on fiber composition, thickness, and additives, so darker areas do not automatically prove higher local mass.
- Capillary flow porometry: Wet and dry flow measurements can characterize connected through-pores in terms of equivalent constriction sizes. They do not directly measure every void or describe the complete three-dimensional network.
- Air permeability and pressure drop: Measurements across several sheet locations reveal consistency under defined conditions. They should be interpreted with specimen area, face velocity or pressure differential, thickness, and conditioning held comparable.
- Filtration testing: Particle penetration and loading behavior establish whether structural differences affect the intended application. Similar pore measurements do not guarantee identical efficiency or service behavior.
For capillary flow porometry, wetting-liquid selection, complete saturation, specimen sealing, and the calculation method affect the result. Bubble-point measurements are particularly sensitive to the largest accessible connected opening, but edge leakage or a handling defect can resemble a material defect. Mean-flow pore size is a different descriptor; it should not be treated as interchangeable with bubble point.
A reported distribution also needs a clear definition. A distribution derived from flow measurements is not necessarily equivalent to a count of openings in a microscope image. Comparing values from different methods without understanding their basis can create an apparent process difference that comes from measurement alone.
Sampling determines whether these measurements describe uniformity. One coupon from the center of a roll cannot establish variation across its width or along its length. A practical plan includes multiple positions and production intervals, with repeat measurements sufficient to distinguish specimen variation from instrument repeatability. Report the spread alongside the average, and investigate isolated extreme results before averaging them away.
How the evidence changes an application decision
Gas-turbine intake media illustrate why pore consistency matters beyond a laboratory distribution. In environments containing fine dust, salt aerosols, and moisture, local open paths may affect particle penetration, while moisture exposure can change resistance and loading behavior. Dispersion is one contributor to this performance; fiber surface properties, layer arrangement, and water management remain separate evaluation requirements.
For wet-laid gradient options within Gas Turbine Intake Filtration, technical assessment should connect formation consistency to finished-filter performance under the intended exposure conditions. A deliberately open upstream layer can support loading capacity, while a finer downstream layer provides additional capture. The relevant question is whether each layer is consistent across its area and whether the combined structure delivers the required performance.
Filter classifications and test standards cannot substitute for that structural evidence. Where ISO 29461 testing is specified, identify the applicable part, procedure, and reported performance. A reference to the standard alone does not demonstrate uniform fiber dispersion, nor does a filtration-class label explain the size or frequency of local formation defects.
The most useful development trial changes a limited number of dispersion variables while keeping fiber composition and finishing conditions comparable. Record fiber length where damage is plausible, check suspension behavior near formation, and measure local sheet variation alongside pore characteristics. Then confirm whether the change improves particle retention and resistance at the required face velocity.
A credible improvement produces a consistent pattern: fewer persistent flocs, less spatial variation, fewer unusually open flow paths, and repeatable filtration performance. If only the average pore value shifts, the trial may have changed packing density without improving uniformity. Further adjustment should follow the location of the remaining variation—suspension preparation, approach flow, drainage, or finishing—rather than treating every pore inconsistency as a request for more mixing.
Recommendation
 Oct 26, 2026
Why pleating trials belong early in filter media development
Filter Media Development benefits from early pleating trials. Discover how to spot cracking, improve pleat stability, and define a reliable process window before specifications are locked.- Oct 26, 2026
When to specify a water-repellent filter media surface treatment
Filter Media Surface Treatment: Learn when water repellency helps protect airflow, how to assess wet performance, and what to specify for reliable industrial filtration. - Oct 26, 2026
How fiber dispersion affects wet-laid nonwoven pore uniformity
Wet-Laid Nonwoven Technology: Discover how fiber dispersion shapes pore uniformity and which process controls and tests can improve filtration consistency.